
 English
 русский
 Português
 Français


 Read More
Product Category
NEW Category
Contact us
Contact Us
We specialise in the research, development and manufacture of electrical wires and cables.
 +86-21-57560276
Hybrid and Direct Contact Heat Exchangers for Efficient Food, Beverage, and Biopharmaceutical Processing
Content
- 1 What Is a Hybrid / Direct Contact Heat Exchanger?
- 2 Operating Principle and Heat Transfer Mechanism
- 3 Key Advantages Compared with Conventional Heat Exchangers
- 4 Construction and Configuration
- 5 Applications in Food and Beverage Manufacturing
- 6 Applications in Biopharmaceutical and Related Industries
- 7 Advantages for Industrial Buyers
- 8 Advanced Manufacturing Processes and Engineering Strengths
- 9 Comparison with Competing Heat Exchange Technologies
- 10 Design Selection Considerations
- 11 Installation, Commissioning, and Operation
- 12 Maintenance and Troubleshooting
- 13 Why Supplier Capability Matters
- 14 Project Workflow from Inquiry to Delivery
- 15 Frequently Asked Questions
- 15.1 Q1: What is the main advantage of a Hybrid / Direct Contact Heat Exchanger?
- 15.2 Q2: Can the equipment replace every shell-and-tube or plate heat exchanger?
- 15.3 Q3: Is direct steam heating suitable for food and beverage processes?
- 15.4 Q4: Can the equipment be used in biopharmaceutical facilities?
- 15.5 Q5: What materials are available?
- 15.6 Q6: Does the equipment require internal tube cleaning?
- 15.7 Q7: Can the shell length and pressure rating be customized?
- 15.8 Q8: What causes uneven outlet temperature?
- 15.9 Q9: How can vibration and water hammer be reduced?
- 15.10 Q10: What information should be provided when requesting a quotation?
- 15.11 Q11: How does the equipment support energy recovery?
- 15.12 Q12: What makes a manufacturer suitable for international projects?
- 16 Conclusion
- 17 References
- 18 Product: Hybrid / Direct Contact Heat Exchanger
Heat exchange is a fundamental operation in food and beverage manufacturing, biopharmaceutical production, chemical processing, environmental engineering, and industrial utilities. Heating, cooling, condensation, waste heat recovery, and temperature conditioning all influence product quality, energy consumption, production capacity, and operating reliability. As manufacturers seek lower utility costs and more flexible process equipment, the limitations of conventional heat exchangers have become increasingly important to address.
Traditional shell-and-tube and plate heat exchangers transfer energy through a metal wall. This indirect arrangement is valuable when two fluids must remain completely separated, but the wall also introduces thermal resistance. Fouling, scaling, corrosion, pressure drop, gasket wear, and difficult cleaning conditions can further reduce performance over time. In applications where the process permits direct contact between the media, a different approach can provide significant technical and economic advantages.
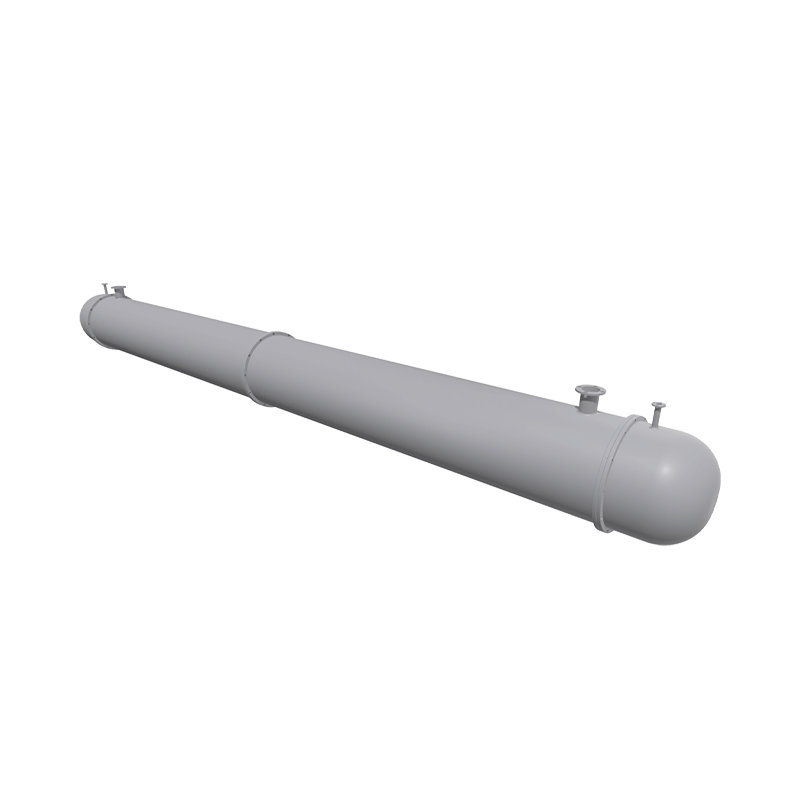
A Hybrid / Direct Contact Heat Exchanger enables hot and cold media to transfer heat through direct contact and controlled mixing. Its horizontal cylindrical shell receives the process media through dedicated inlets, allowing the streams to interact inside a pressure-resistant vessel. Depending on the process design, the equipment can support heating, cooling, condensation, gas treatment, or energy recovery while combining media mixing and heat transfer in one operating step.
This article explains the operating principle, construction, advantages, applications, design considerations, manufacturing capabilities, and service strengths associated with Hybrid / Direct Contact Heat Exchangers. It also examines how advanced manufacturing, material selection, quality control, and process engineering can improve the value of this equipment for food, beverage, biopharmaceutical, and related industries.
Hybrid / Direct Contact Heat Exchanger
What Is a Hybrid / Direct Contact Heat Exchanger?
A Hybrid / Direct Contact Heat Exchanger is process equipment designed to transfer heat directly between two media that are permitted to mix. Unlike an indirect heat exchanger, it does not depend exclusively on a tube wall, plate, or other separating surface between the hot and cold streams. Instead, heat moves directly from one medium to another through physical contact.
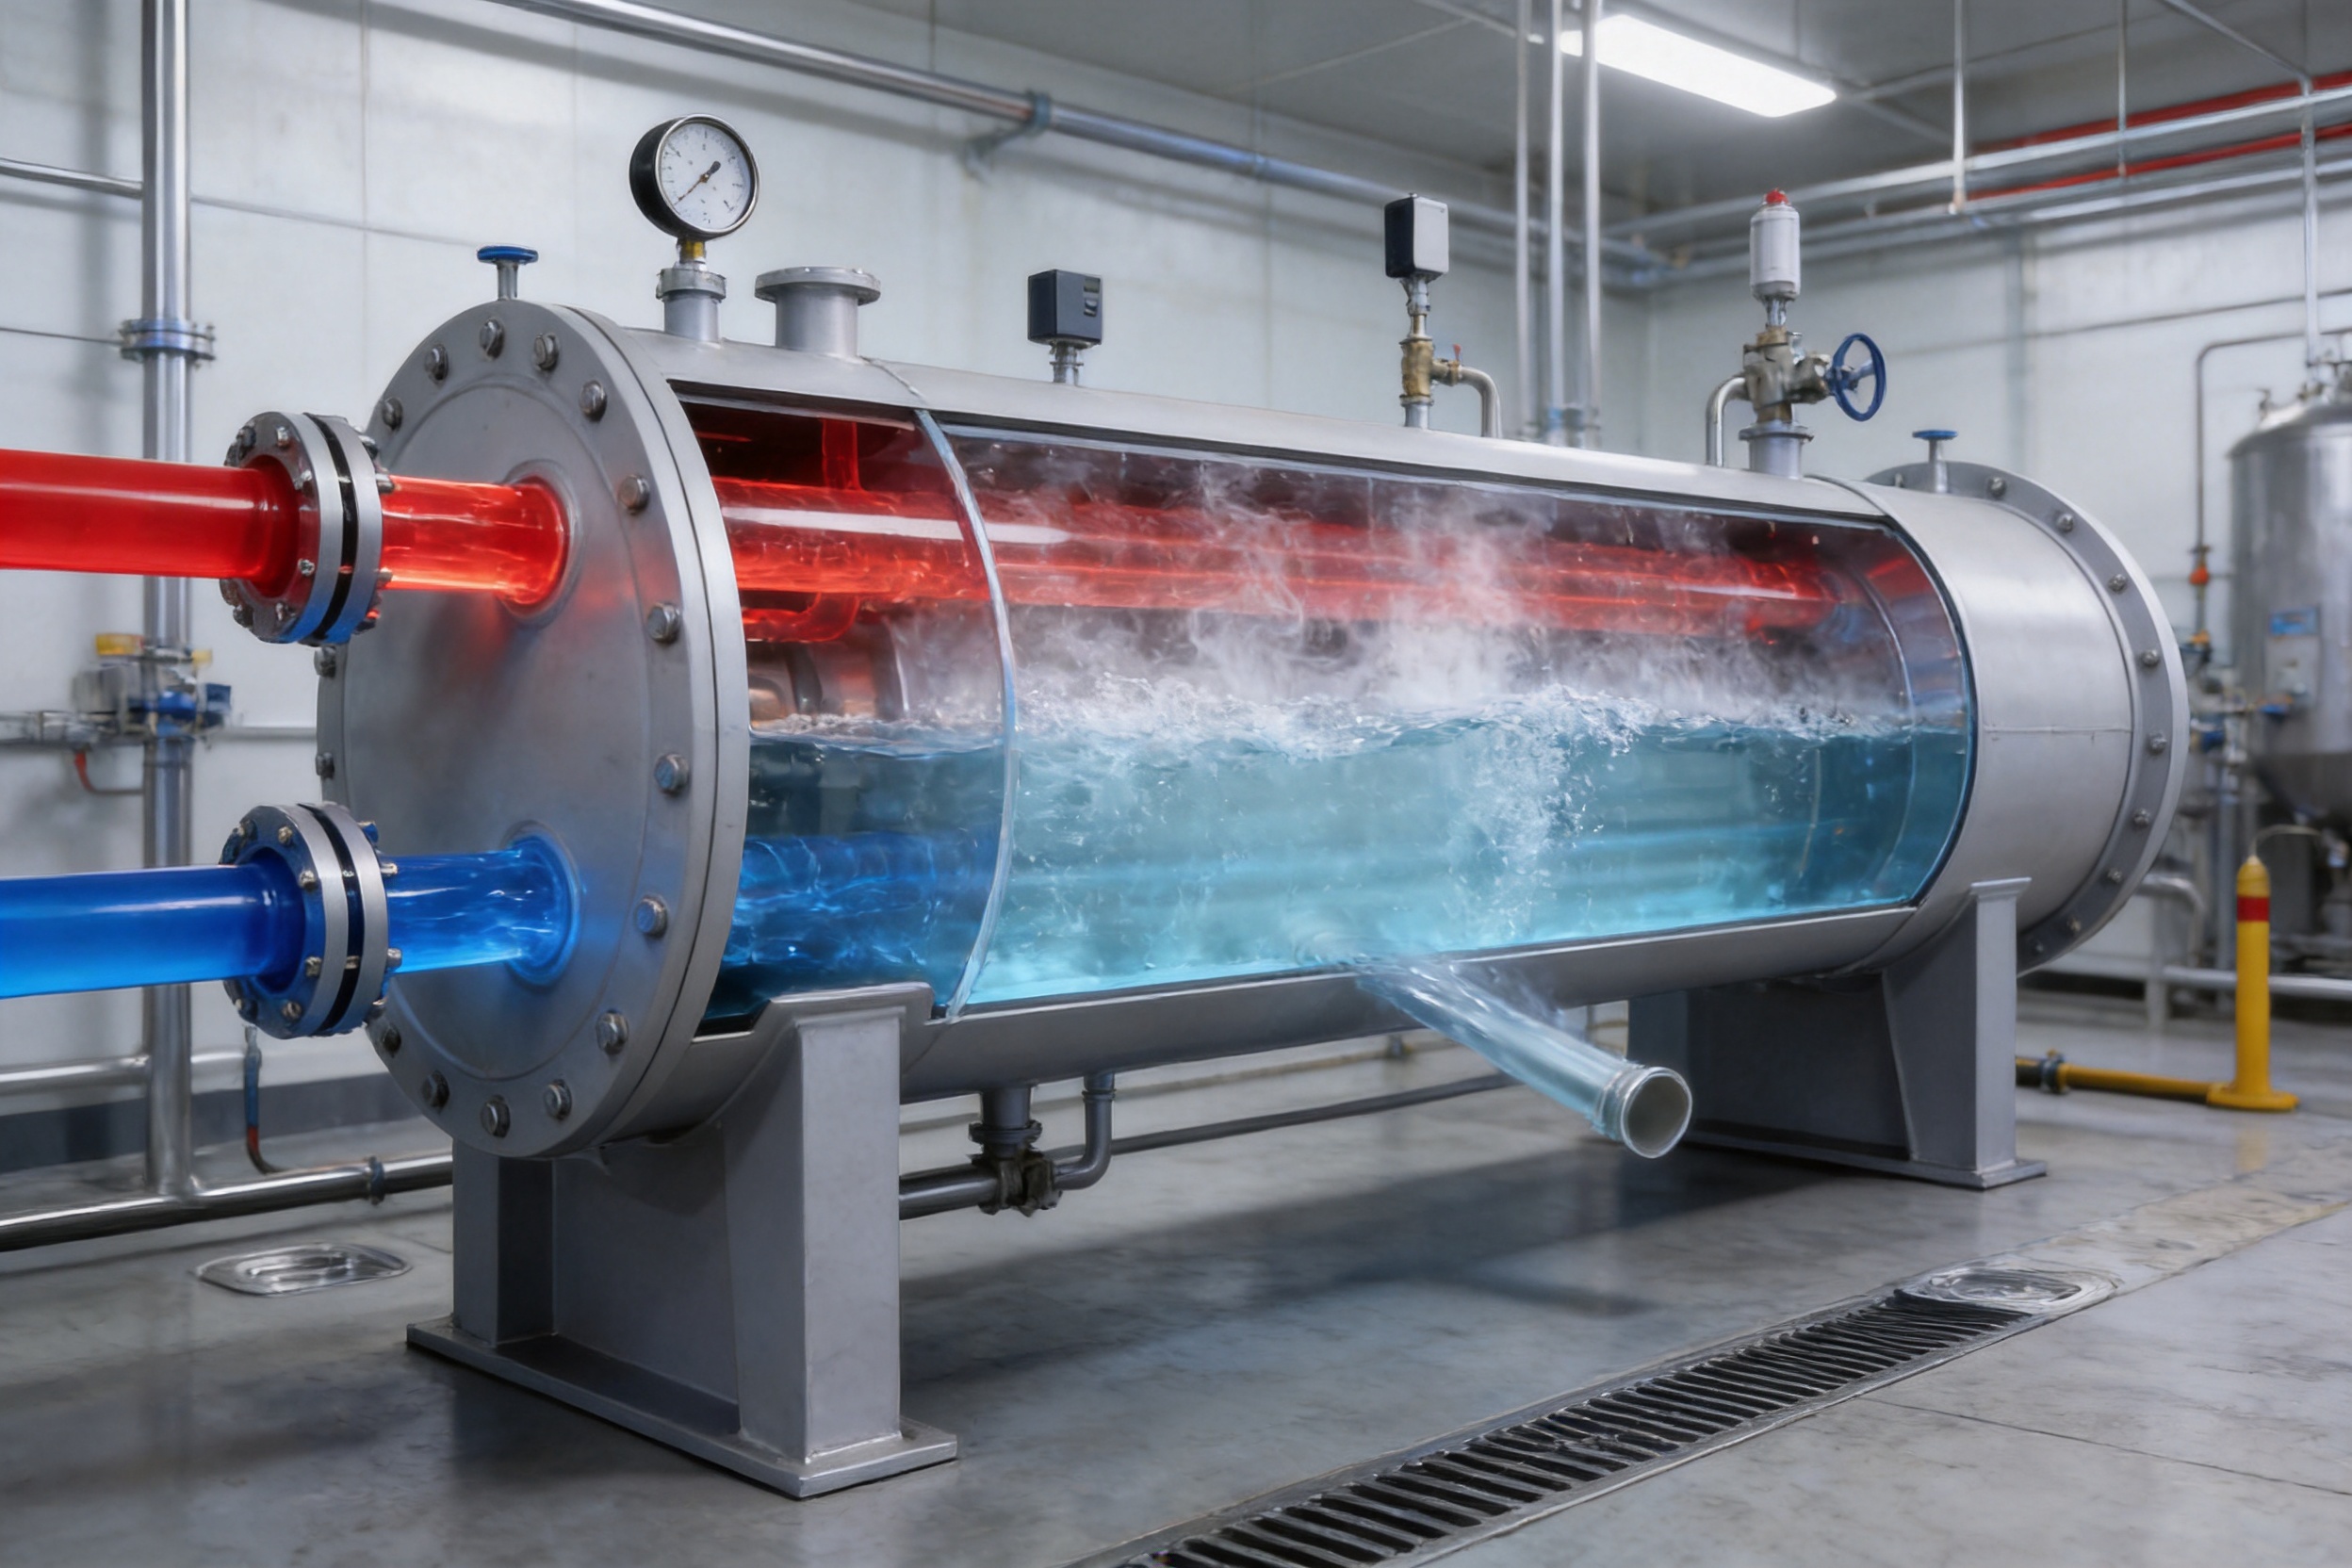
The equipment typically uses a horizontal, long cylindrical shell. One or more media enter through flanged connections and are distributed according to the process requirements. When hot and cold streams meet inside the shell, sensible heat is transferred rapidly. In steam and water applications, steam may condense directly into the water. In gas treatment applications, a liquid may directly contact a hot gas to cool it, absorb soluble components, or support scrubbing.
The term “hybrid” describes the ability to combine direct contact functions with other process arrangements when required. A system may include upstream or downstream indirect heat exchangers, separators, pumps, spray devices, condensate recovery equipment, control valves, or filtration units. This allows engineers to use direct contact where it is most beneficial while maintaining fluid separation in sections where product purity, formulation, or process safety requires it.
The primary condition for direct contact operation is compatibility between the media. The streams must be suitable for mixing, or the process must include a reliable separation or recovery step after heat transfer. For example, direct steam heating is appropriate when condensed steam can become part of the process water or can be recovered within the utility system. It is not automatically suitable for every product stream. Media identity, purity, chemical compatibility, regulatory requirements, and downstream separation must be evaluated before final design approval.
Operating Principle and Heat Transfer Mechanism
In an indirect heat exchanger, energy moves from a hot fluid through a metal wall and then into a cold fluid. Every layer contributes thermal resistance. The total resistance depends on the fluid film coefficients, the wall material and thickness, surface deposits, and the flow arrangement. As fouling accumulates, the effective heat transfer coefficient decreases and the equipment may require greater temperature differences or longer operating time.
Direct contact heat transfer eliminates the separating wall between compatible media. When the streams meet, the available contact area can be much greater than the geometric surface area of a conventional tube bundle. Turbulence, droplet formation, condensation, and mixing expose fresh fluid surfaces to one another, supporting fast energy transfer. The process can therefore achieve effective heating or cooling in a relatively compact vessel.
For direct steam heating, steam enters the shell and contacts water or another compatible liquid. The steam condenses as its latent heat is released. The condensate becomes part of the liquid phase, which can be advantageous when the added water is acceptable and steam quality is appropriately controlled. In a condensation and recovery system, the equipment can support the capture and return of condensate to improve utility efficiency.
For high-temperature gas cooling, a liquid is introduced into the gas stream or into the shell in a controlled pattern. The liquid absorbs sensible heat from the gas. Depending on the process, it may also absorb soluble contaminants. This makes the equipment useful for waste gas cooling and certain scrubbing arrangements, although gas composition, corrosion resistance, pressure drop, mist elimination, and wastewater treatment must be considered as part of the complete system.
The actual heat transfer performance depends on flow rate, inlet temperature, pressure, media properties, contact pattern, residence time, mixing intensity, and outlet temperature. The inlet arrangement is therefore not a minor detail. Injection angle, nozzle configuration, flow distribution, and the ratio of hot to cold media all influence the uniformity of the final temperature and the risk of localized condensation, vibration, or water hammer.
Key Advantages Compared with Conventional Heat Exchangers
Reduced Thermal Resistance
The most important advantage of direct contact operation is the removal of the conventional heat transfer wall. Since heat does not need to pass through a tube or plate, the thermal resistance associated with that surface is substantially reduced. The result can be faster heating or cooling, improved energy utilization, and a smaller temperature driving force for a given duty.
This advantage is especially relevant when a process requires rapid temperature adjustment or when the temperature difference between the two streams is limited. Instead of increasing the exchanger surface area, adding more tube passes, or using a larger plate pack, engineers may achieve the required duty through controlled direct mixing.
Integrated Mixing and Heat Exchange
A conventional heat exchanger transfers heat but normally does not provide complete mixing of the two fluids. Separate mixers, static mixers, tanks, or recirculation loops may be necessary. A Hybrid / Direct Contact Heat Exchanger combines the two functions in one process vessel when the media can be mixed safely.
Integrated operation can simplify the process line, reduce the number of equipment items, and decrease the footprint of the utility area. Fewer components may also reduce installation time and the number of potential leakage points. In a well-designed system, the equipment can provide thermal conditioning and composition adjustment at the same time.
Simple Internal Structure
Many conventional heat exchangers contain tube bundles, plates, seals, baffles, support grids, or narrow flow passages. These components are essential for indirect heat transfer, but they may create areas where solids, fibers, crystals, or viscous materials accumulate. They can also make inspection, mechanical cleaning, and repair more complicated.
The direct contact design uses a pressure-resistant shell and media distribution arrangements rather than a large internal tube bundle. The simpler structure can lower the risk of fouling caused by narrow passages. It may also make internal inspection more straightforward. However, simple structure does not mean that engineering details can be ignored. Inlet distribution, shell geometry, drainage, supports, weld quality, and access for maintenance remain critical.
Adaptability to Impurities and Difficult Media
When a process contains suspended particles or media that would quickly foul a tube bundle, the absence of small internal passages can be a significant benefit. The equipment can be configured for process water, steam, gases, and other fluids that are directly mixable. Material selection and velocity control must still be matched to the specific contaminants and corrosion risks.
Direct contact technology may also be useful for certain high-viscosity or particulate-containing applications where a conventional exchanger would require frequent cleaning. This does not mean that every difficult medium is automatically suitable. Viscosity, density, particle size, phase behavior, chemical reactivity, and separation requirements must be assessed during process design.
Compact and Flexible Process Integration
The horizontal cylindrical shell can be designed in different length, diameter, pressure, and material configurations. This flexibility allows the equipment to fit different flow capacities and plant layouts. Flanged connections support integration with standard industrial piping, valves, pumps, instrumentation, and control systems.
Compared with an oversized indirect heat exchanger, a direct contact unit may require less heat transfer surface area. Reduced equipment size can support more efficient use of production space, particularly in utility rooms, skid systems, and retrofit projects. The final footprint depends on residence time, separation equipment, maintenance clearance, and process safety requirements.
Potentially Lower Maintenance Burden
Tube fouling, plate gasket damage, tube leakage, and plate pack cleaning are common maintenance concerns for conventional heat exchangers. A direct contact unit avoids many of these specific failure modes because it does not rely on a large tube bundle or a broad gasketed plate pack for heat transfer.
Routine inspection is still necessary. Shell connections, welds, supports, inlet devices, drains, valves, and instrumentation must be checked. Deposits may develop inside the vessel depending on the media, and corrosion can occur if material selection or water chemistry is unsuitable. The main difference is that maintenance focuses on a pressure vessel and distribution system rather than a complex internal heat transfer matrix.
Construction and Configuration
Horizontal Cylindrical Shell
The main body is a horizontal cylindrical shell designed to contain the process pressure and provide sufficient contact volume. The shell length, diameter, wall thickness, and support arrangement are selected according to design pressure, design temperature, flow rate, residence time, media density, and applicable codes or customer specifications.
A horizontal arrangement can support stable installation on structural saddles or frames. It may also provide a practical flow path for gas, steam, water, and mixed phases. Drainage and venting should be considered carefully so that the vessel does not retain unwanted liquid or gas during shutdown and maintenance.
Media Inlets and Distribution
Media are introduced through flanged inlet connections. The position and orientation of each inlet influence mixing quality, pressure drop, noise, vibration, and temperature distribution. Depending on the application, the design may use direct inlet nozzles, internal distribution devices, spray arrangements, or other flow-guiding components.
The inlet design must prevent excessive local velocity and avoid uncontrolled impingement on the shell wall. It should also promote sufficient contact without generating unnecessary turbulence. For steam applications, the distribution pattern should help prevent water hammer and uneven condensation. For gas applications, the system should support adequate liquid contact while limiting entrainment and downstream carryover.
Outlet and Drainage Arrangement
The outlet configuration depends on whether the process produces a mixed liquid, cooled gas, condensate, or a combination of phases. A liquid outlet may require a level control arrangement, while a gas outlet may need a demister or downstream separator. Condensate recovery systems may include dedicated drains, collection vessels, pumps, and return lines.
Drainage is important for hygiene, corrosion prevention, freeze protection, and maintenance. Low points should be evaluated to avoid dead zones where product or process liquid can remain after shutdown. For food and biopharmaceutical applications, the design should be reviewed against the required cleaning, sanitization, and contamination-control strategy.
Materials of Construction
Carbon steel may be suitable for selected utility, water, or gas applications where the media are not corrosive and surface requirements are moderate. Stainless steel is generally preferred when the process involves corrosive fluids, higher hygiene expectations, or contact with food and pharmaceutical-related materials. The specific grade should be selected based on chloride concentration, pH, temperature, cleaning chemicals, mechanical requirements, and applicable regulations.
Material choice should include the shell, nozzles, internal distribution devices, flanges, welds, gaskets, valves, and instruments. A mismatch between the shell material and auxiliary components can create localized corrosion or contamination risks. Surface finish, weld profile, passivation, and traceability may be important for hygienic service.
Pressure and Temperature Design
The pressure-resistant shell is designed to adapt to specified operating conditions. Pressure and temperature ratings should not be selected only from normal operating values. Design conditions must account for start-up, shutdown, blocked outlets, steam surges, pressure fluctuations, vacuum conditions, thermal expansion, and possible water hammer.
The equipment should be protected by appropriate relief devices and control systems. Temperature and pressure transmitters can provide process feedback, while automatic valves regulate steam, water, gas, or condensate flow. Interlocks may be used to prevent operation outside the approved pressure, temperature, or level range.
Applications in Food and Beverage Manufacturing
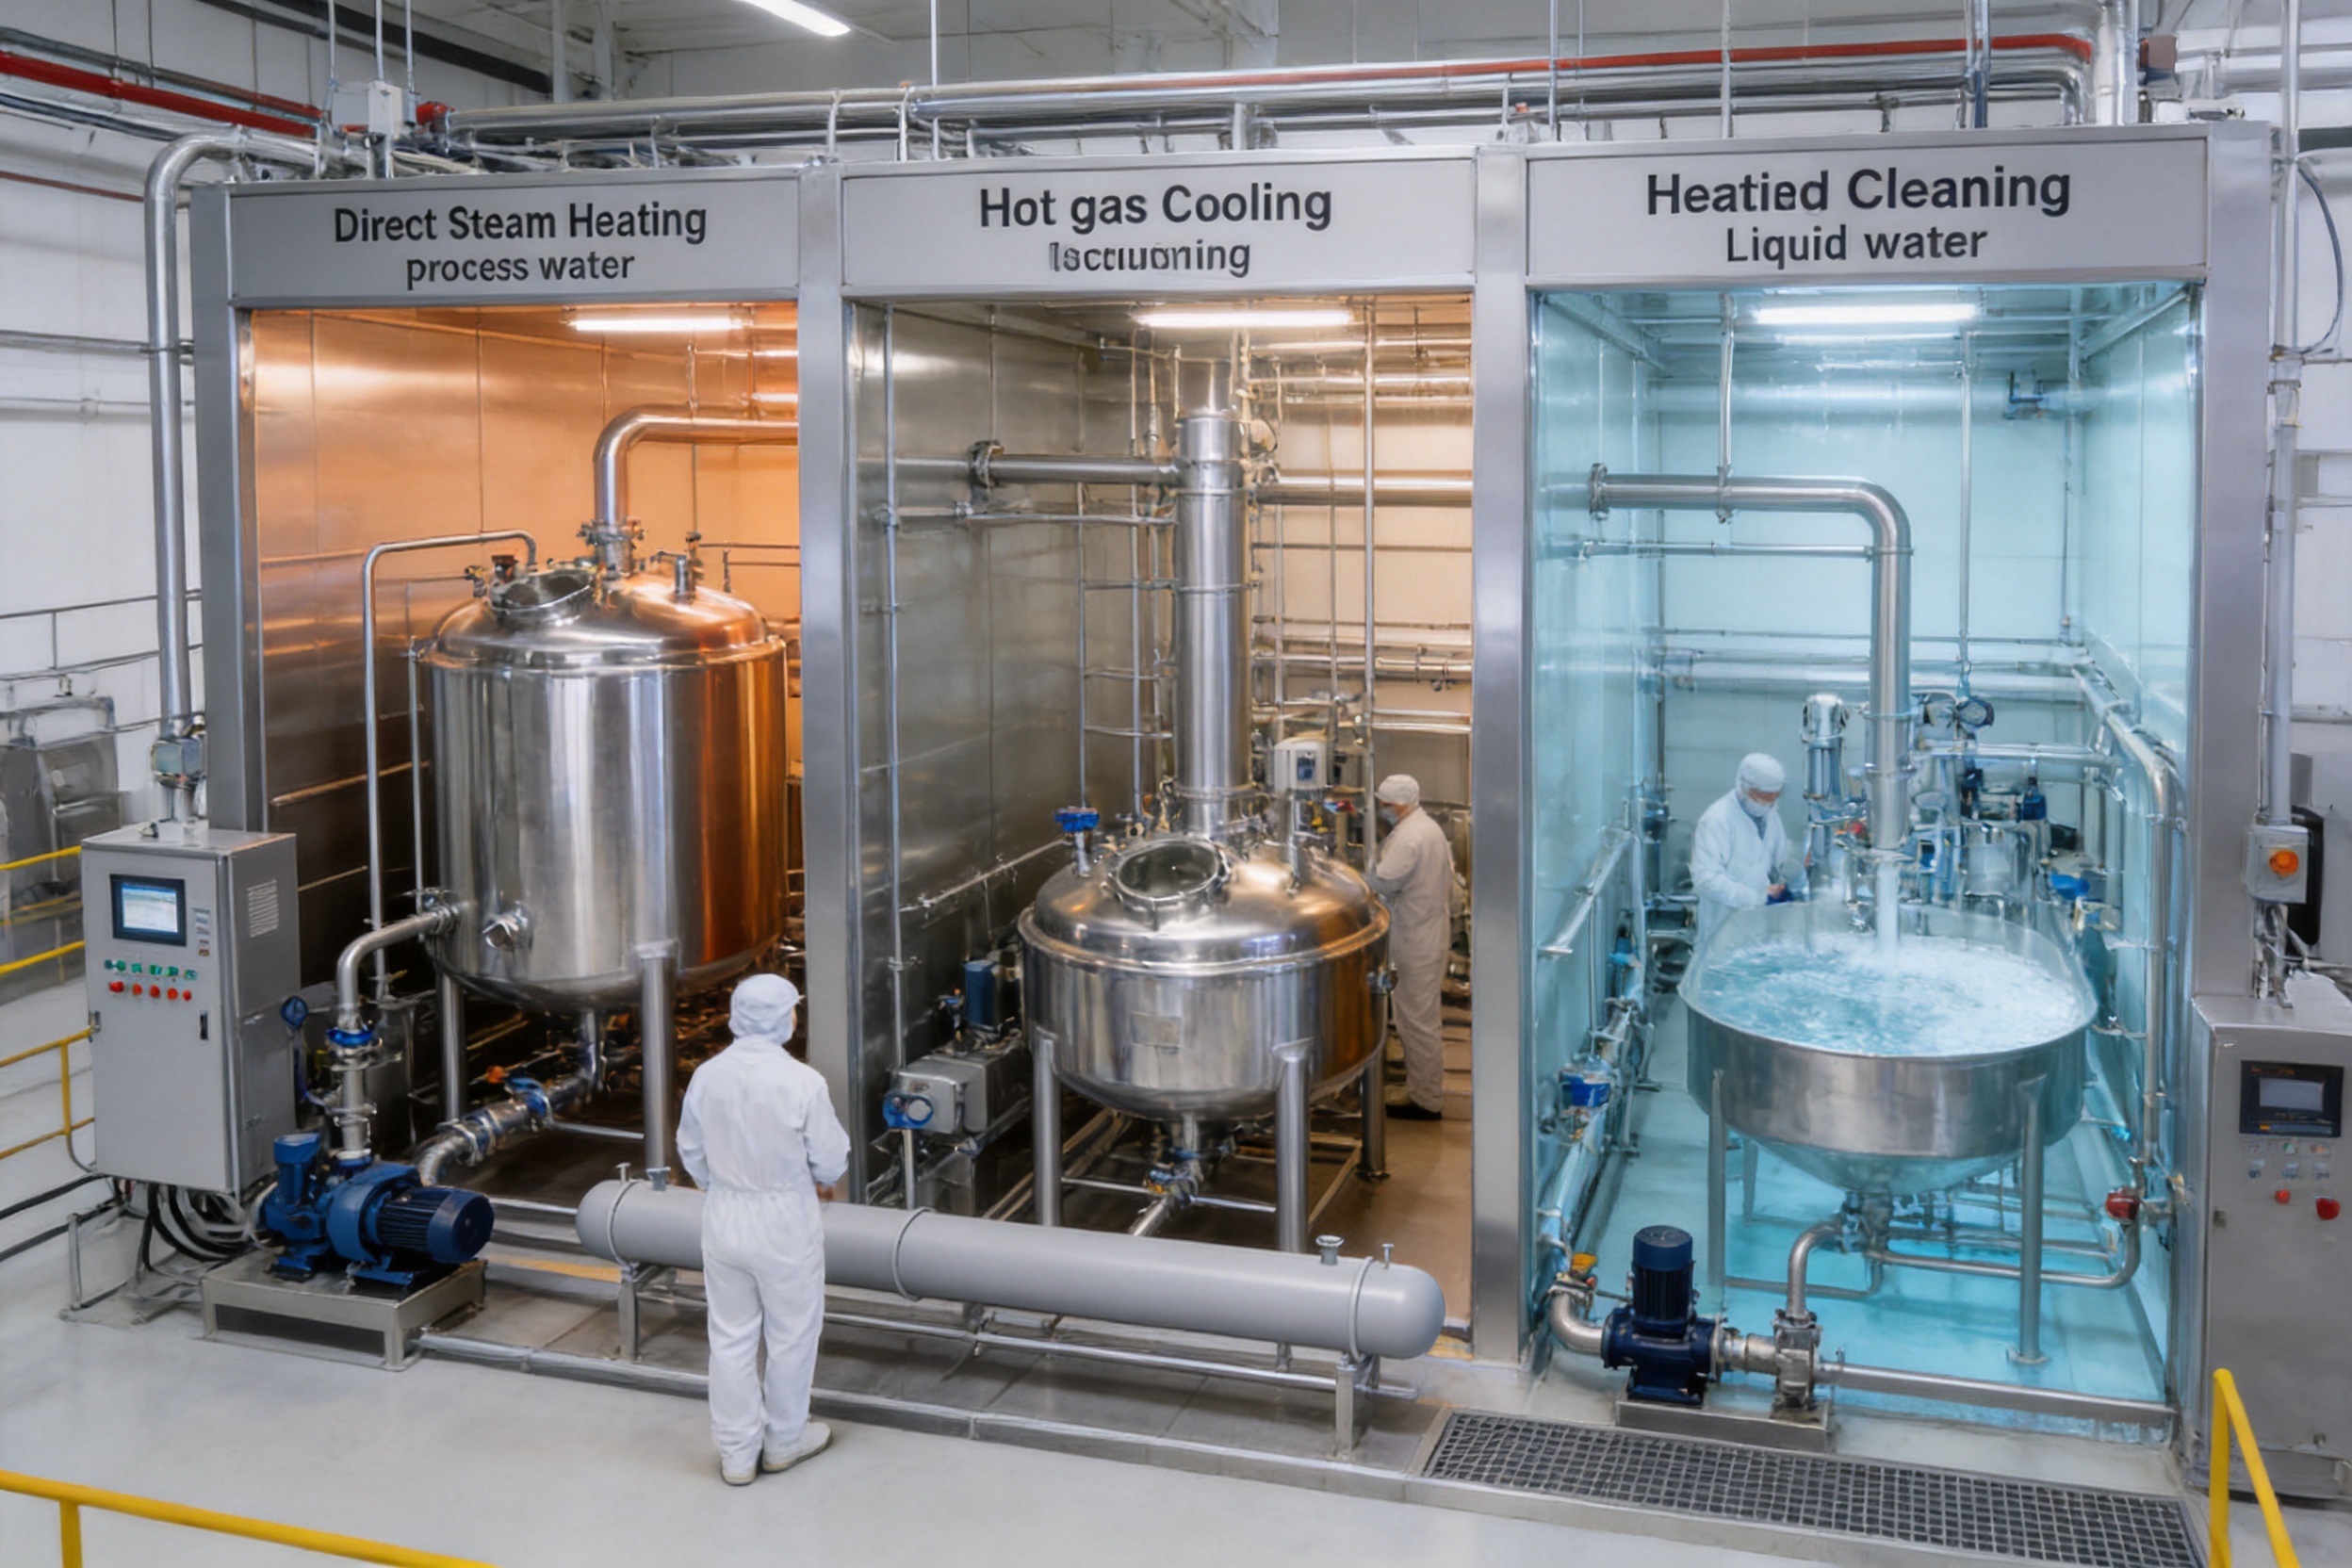
Direct Steam Heating of Process Water
Food and beverage plants use substantial quantities of hot water for processing, cleaning, rinsing, extraction, and utility operations. Direct steam heating can quickly raise the water temperature without requiring a separate hot-water loop or a large indirect exchanger. The condensed steam becomes part of the water stream when the steam quality and process specification permit it.
This arrangement can reduce response time during demand changes. It may also reduce the amount of equipment required between the boiler system and the point of use. Accurate temperature control remains essential, especially when the water is used in a product-related step or in a cleaning process with defined thermal requirements.
Condensation and Condensate Recovery
Steam condensation systems can recover thermal energy and reduce utility losses. The direct contact exchanger supports contact between steam and a compatible liquid or recovery stream. The recovered condensate may be routed to a collection or boiler feedwater system after suitable quality checks and treatment.
Condensate recovery design should consider non-condensable gases, contamination risk, pressure fluctuations, flash steam, and return-line backpressure. The exchanger is one part of the overall recovery system and should be coordinated with pumps, separators, control valves, traps, tanks, and monitoring equipment.
Waste Gas Cooling and Scrubbing
High-temperature exhaust gas may need to be cooled before entering a filter, scrubber, fan, or emission-control system. Direct contact with water or another suitable liquid can rapidly lower the gas temperature. If the liquid also absorbs soluble substances, the same operation may contribute to gas scrubbing.
Waste gas applications require careful analysis of gas chemistry, condensate composition, corrosion potential, aerosol formation, and wastewater handling. Stainless steel, protective coatings, or specialized alloys may be required. The design should also address downstream mist removal to prevent liquid carryover.
Heating and Cooling of Ingredient or Utility Streams
In some food processes, direct contact is suitable for water-based ingredients or utility streams where the addition of the heating or cooling medium is acceptable. The equipment may support temperature conditioning before blending, extraction, washing, or cleaning. It can be integrated with pumps, tanks, flowmeters, and automated temperature control loops.
Direct contact should not be selected solely because it offers fast heat transfer. If the process requires strict separation of utilities from the product, an indirect sanitary exchanger may be more appropriate. A process engineer should confirm whether mixing is acceptable and whether the final composition remains within the product specification.
Applications in Biopharmaceutical and Related Industries
Utility and Process Water Systems
Biopharmaceutical facilities require carefully controlled water systems for production, cleaning, sterilization support, and facility utilities. A Hybrid / Direct Contact Heat Exchanger may be considered for suitable utility-water applications where direct steam contact is allowed and the steam quality is controlled. The system must be evaluated against the facility’s water classification, validation strategy, and contamination-control requirements.
For high-purity product-contact water, the choice between direct and indirect heating requires particularly rigorous review. Materials, surface finish, drainability, cleanability, steam quality, microbial control, and documentation may be more important than the nominal heat transfer rate. In many cases, a customized design or an indirect sanitary solution will be preferred for the final product-contact step.
Cleaning and Sanitization Support
Cleaning-in-place and sanitization systems often require controlled heating of water or cleaning solutions. Where direct mixing is compatible with the cleaning formulation, the equipment can rapidly prepare a heated utility stream. This can support responsive operation and reduce the size of hot-water storage systems.
The cleaning sequence should define the acceptable materials, chemical concentrations, temperature limits, flow rates, and drainage conditions. The exchanger should be installed so that it can be inspected and maintained without compromising the validated cleaning process.
Process Development and Pilot Systems
Pilot plants and process development facilities frequently require flexible equipment that can accommodate changing flow rates and different operating conditions. The configurable shell length, pressure rating, material selection, and inlet arrangement of a direct contact unit can support development work when the media are compatible.
For scale-up, laboratory or pilot data should be used to confirm mixing behavior, residence time, phase separation, temperature uniformity, and energy balance. Direct contact performance may change with scale because of differences in velocity, nozzle behavior, gas distribution, and vessel geometry. A reliable supplier should support engineering review rather than simply replicate dimensions.
Advantages for Industrial Buyers
For equipment buyers, the value of a heat exchanger extends beyond the initial purchase price. Total cost of ownership includes energy consumption, installation, spare parts, cleaning, downtime, inspection, operator workload, and equipment life. The Hybrid / Direct Contact Heat Exchanger can create value in several of these areas when applied to a suitable process.
First, improved heat transfer can reduce the amount of steam or cooling utility required for a given duty. Actual savings depend on operating conditions and the efficiency of the complete utility system, but eliminating wall resistance can improve the thermal balance.
Second, the integrated mixing function can reduce the need for separate equipment. A simpler process train may require fewer pumps, tanks, mixers, and interconnecting lines. This can reduce capital cost and simplify plant layout, although any required separator, filter, or recovery system must be included in the total project estimate.
Third, the absence of a large tube bundle or plate pack can simplify maintenance. Operators may spend less time opening, cleaning, and reassembling heat transfer surfaces. Reduced fouling risk may also improve production availability in applications containing suspended solids or other challenging materials.
Fourth, the equipment can be customized around the process rather than forcing the process to fit a standard exchanger. Pressure ratings, shell materials, length, connection locations, media distribution, and instrumentation can be selected according to the customer’s requirements.
Finally, a well-engineered direct contact system can provide a practical solution for heat recovery. Waste heat from steam, condensate, exhaust gas, or another process stream may be transferred directly to a compatible receiving medium, reducing the loss of useful energy.
Advanced Manufacturing Processes and Engineering Strengths
The performance and reliability of a pressure-resistant process vessel depend heavily on manufacturing quality. A sound design can fail to deliver its expected service life if forming, welding, polishing, inspection, or assembly is poorly controlled. Advanced manufacturing processes are therefore a central part of the equipment’s value.
Engineering Review and Process Customization
Manufacturing should begin with a structured review of the customer’s process conditions. Important inputs include media composition, flow rate, inlet and outlet temperatures, pressure, phase behavior, corrosion potential, cleaning chemicals, required materials, available utilities, installation location, and applicable standards.
Process engineers can use these inputs to determine the shell dimensions, inlet arrangement, residence volume, connection sizes, support configuration, material grade, pressure class, and instrumentation requirements. This front-end engineering reduces the risk of selecting an exchanger that performs well in theory but poorly under actual plant conditions.
Customization is particularly important for direct contact equipment because mixing quality depends on geometry. The inlet angle, nozzle position, and relative flow rates can influence temperature distribution and operating stability. Engineering review should also consider start-up, shutdown, emergency drainage, maintenance access, and integration with control systems.
Precision Fabrication and Forming
The cylindrical shell and end components require accurate forming and fit-up. Dimensional control helps maintain alignment between shell sections, nozzles, flanges, supports, and internal distribution elements. Accurate fabrication also reduces stress concentrations and simplifies installation in a prefabricated skid or plant piping system.
Where stainless steel is used, fabrication procedures should control contamination from carbon-steel tools, embedded particles, and unsuitable abrasives. Dedicated tools, appropriate storage, and controlled handling help protect the surface condition of the finished equipment.
High-Quality Welding
Welding is one of the most important manufacturing operations for a pressure-bearing shell. Qualified welding procedures, trained operators, controlled heat input, suitable filler materials, and proper joint preparation contribute to mechanical integrity and corrosion resistance.
For hygienic or high-purity applications, weld profile and internal smoothness are especially important. Poorly finished welds can create crevices that retain product, cleaning chemicals, or microorganisms. Orbital welding or other controlled techniques may be considered for selected connections, while manual welding can be used where appropriate under documented procedures.
Weld inspection may include visual examination, dimensional inspection, dye penetrant testing, radiographic testing, ultrasonic testing, pressure testing, or other methods required by the design code and customer specification. The inspection plan should be established before fabrication rather than added after production.
Polishing and Surface Treatment
Stainless-steel surfaces may require grinding, polishing, passivation, or electropolishing depending on the application. A controlled surface finish can improve cleanability and reduce the likelihood of deposit formation. It can also support more consistent sanitation procedures in food, beverage, and biopharmaceutical environments.
Surface treatment must be compatible with the selected material and process. Passivation can help restore the protective oxide layer after fabrication, while proper rinsing removes chemical residues. Surface-finish records and inspection results may form part of the equipment documentation package.
Dimensional and Pressure Testing
Completed equipment should be checked against approved drawings. Nozzle orientation, flange alignment, support dimensions, shell length, access openings, drain locations, and instrument connections should be verified before shipment.
Pressure testing confirms the integrity of the pressure boundary. Hydrostatic testing is commonly used when suitable, while alternative testing methods may be considered according to the design and customer requirements. Testing should be performed with calibrated instruments and documented results. After testing, the equipment should be drained, dried, preserved, and protected against contamination or corrosion during storage and transport.
Quality Control and Traceability
A professional manufacturer should maintain traceability for materials, welding consumables, inspection records, pressure tests, surface treatment, and final release. Documentation may include material certificates, welding procedure records, welder qualifications, inspection reports, pressure-test certificates, dimensional reports, assembly drawings, operation manuals, and spare-parts lists.
Traceability is valuable for both regulatory compliance and long-term maintenance. If a replacement flange, gasket, nozzle, or internal component is required several years after installation, accurate records make it easier to identify the correct specification.
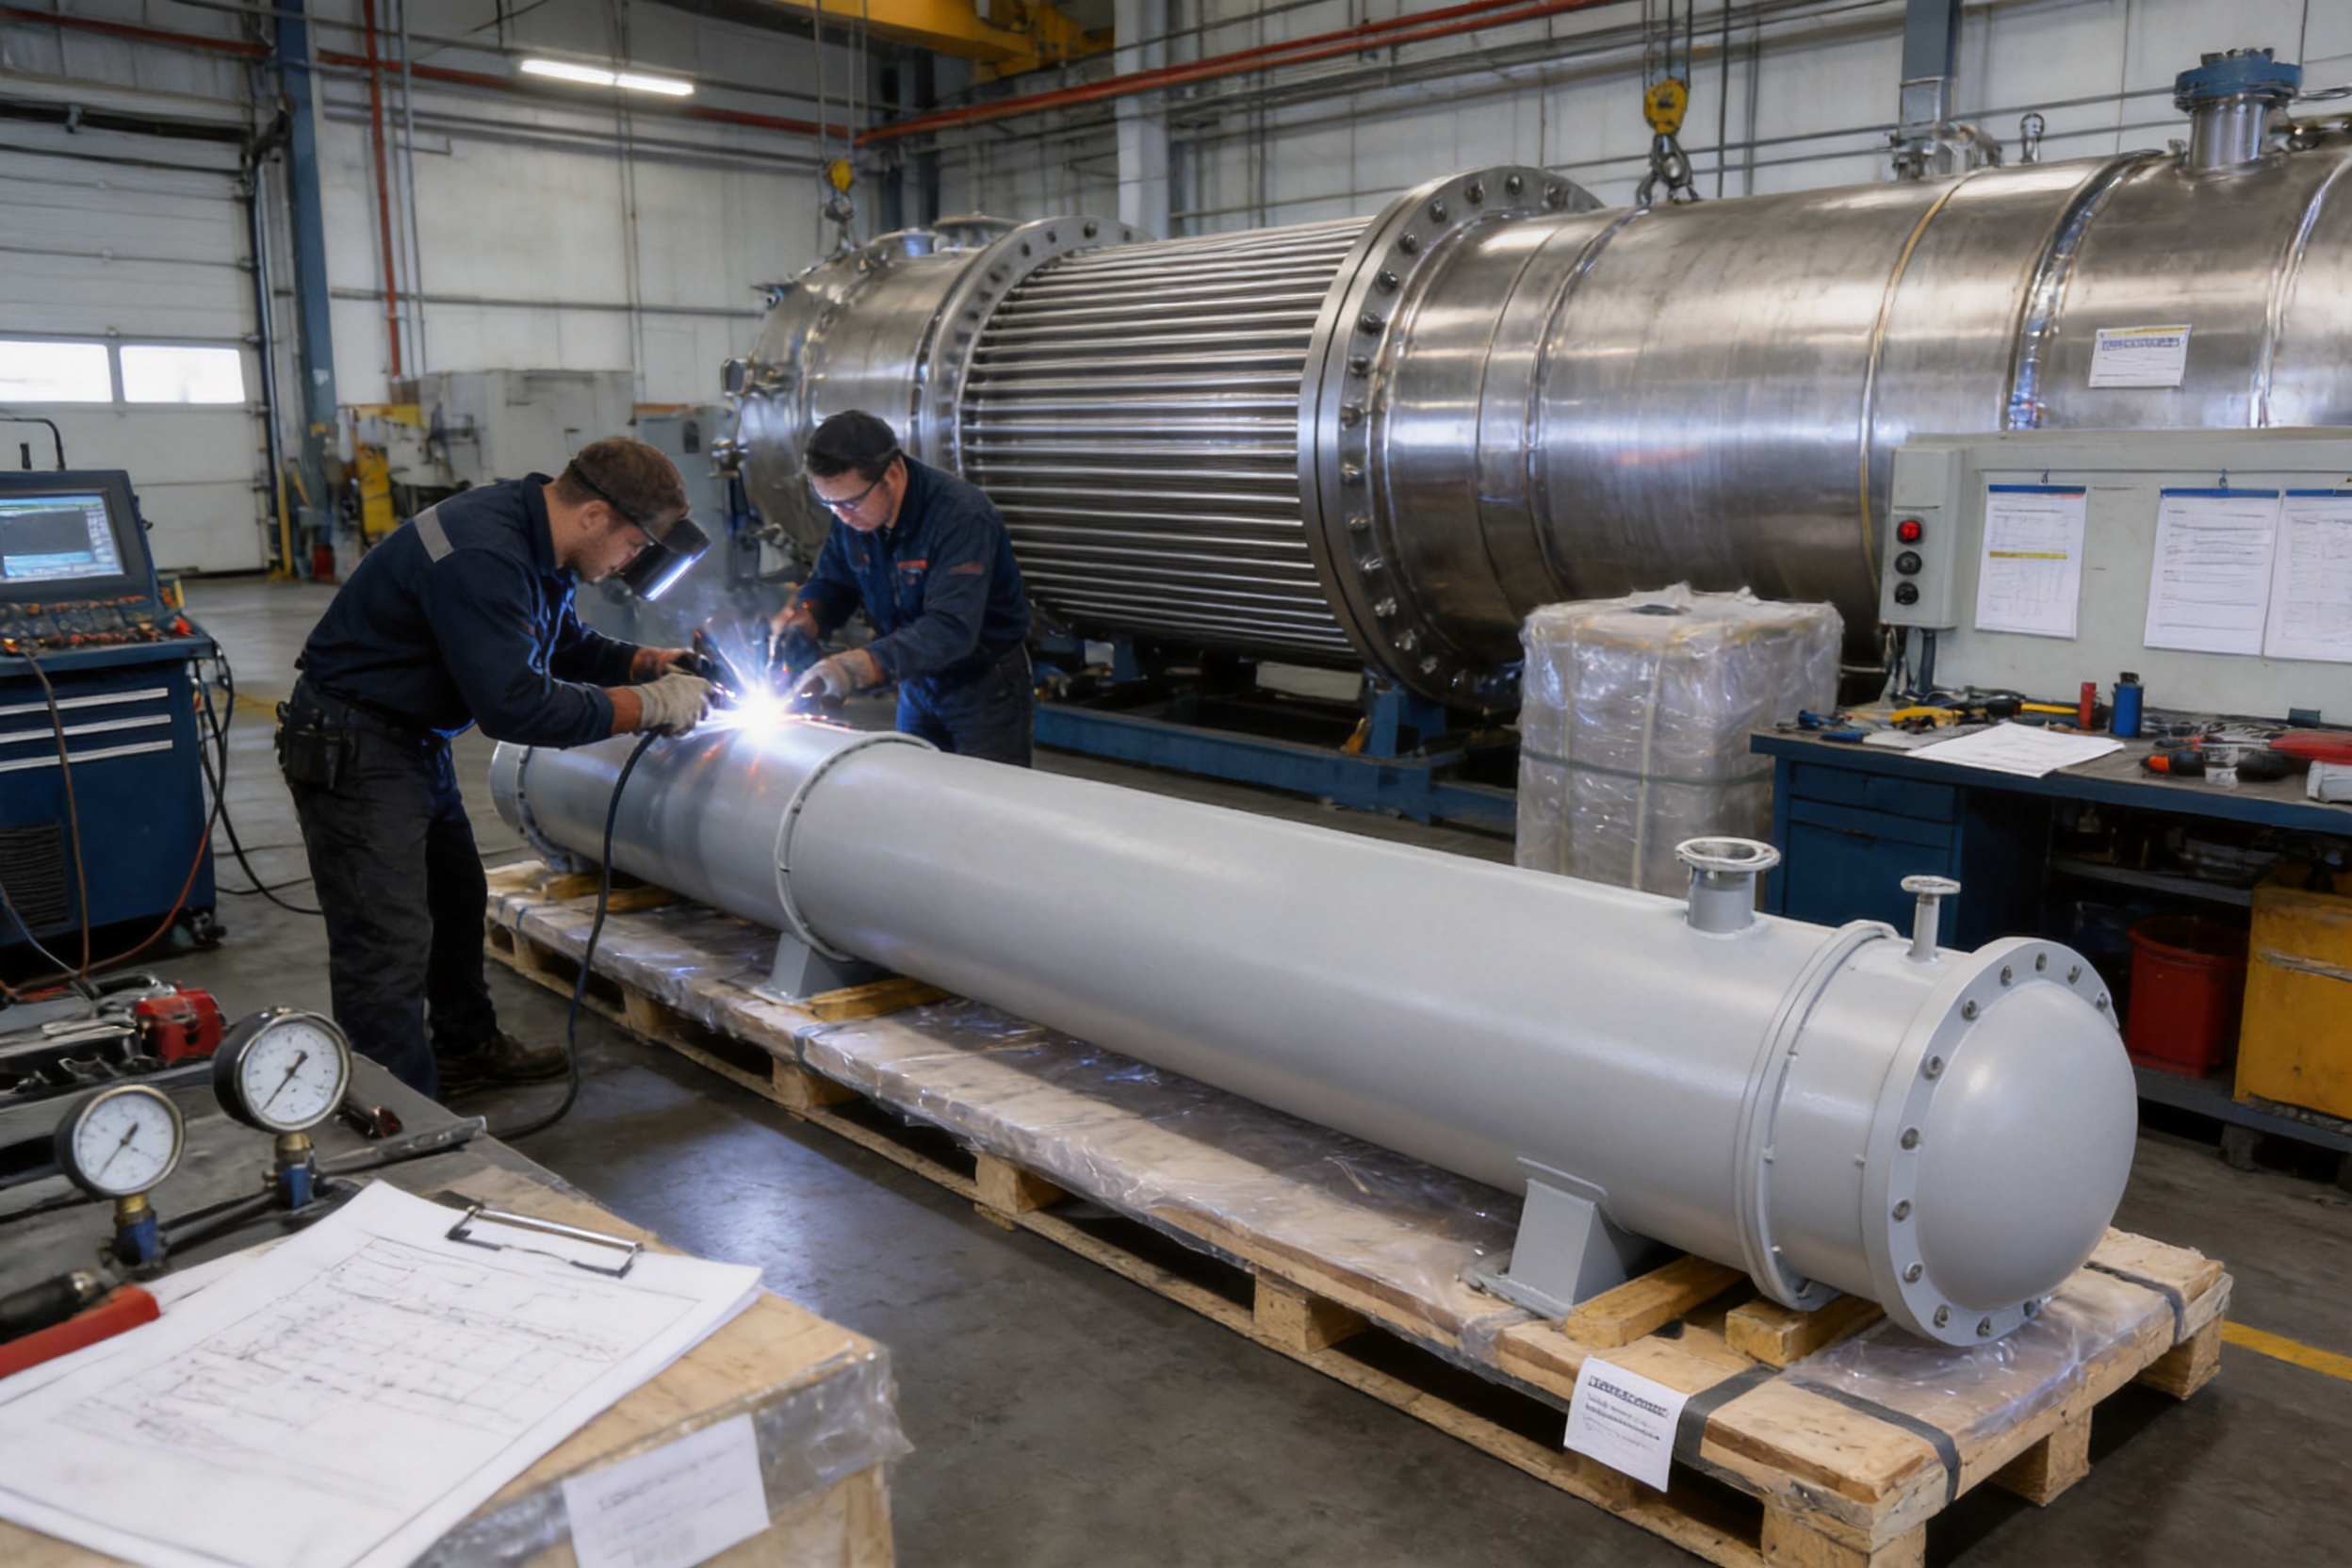
Shiloc (Shanghai) Industrial Trading Co., Ltd. combines equipment manufacturing with international trade, engineering, and technical service capabilities. Its Shanghai facility covers approximately 3,000 square meters and includes capabilities for processing, welding, polishing, and quality control. A technical team of more than 20 specialists supports design communication, production coordination, inspection, and customer requirements.
The company’s approach is based on European know-how and Danish design principles, combined with local manufacturing and project execution. This combination can help international customers obtain customized equipment while receiving support with procurement, technical coordination, documentation, logistics, and cross-border communication.
Comparison with Competing Heat Exchange Technologies
| Evaluation Factor | Hybrid / Direct Contact Heat Exchanger | Shell-and-Tube Heat Exchanger | Plate Heat Exchanger |
|---|---|---|---|
| Heat transfer mechanism | Direct contact and mixing between compatible media | Indirect transfer through tube walls | Indirect transfer through thin plates |
| Media separation | Media may mix; compatibility is essential | Hot and cold streams remain separated | Hot and cold streams remain separated |
| Thermal resistance | Low resistance because no primary transfer wall is required | Includes tube-wall and fouling resistance | Includes plate-wall and fouling resistance |
| Internal complexity | Generally simple shell and distribution arrangement | Tube bundle, supports, and baffles | Plate pack, gaskets, and clamping frame |
| Fouling considerations | Fewer narrow passages, but deposits may still occur in the shell | Tube fouling can reduce performance and increase cleaning frequency | Small passages and gasket areas may require careful cleaning |
| Mixing function | Integrated with heat transfer | Normally requires separate equipment | Normally requires separate equipment |
| Typical strengths | Fast heating, cooling, condensation, gas cooling, and heat recovery | Broad range of separated-fluid applications and high pressure duties | Compact size and high efficiency for clean separated fluids |
| Main limitation | Not suitable when media must remain completely separated | Can be larger and more difficult to clean in fouling service | May be sensitive to fouling, gasket limitations, and pressure constraints |
This comparison does not mean that direct contact equipment replaces all other heat exchanger types. Shell-and-tube and plate exchangers remain essential when fluids must be separated, when cross-contamination cannot be tolerated, or when the process requires a specific sanitary or pressure arrangement. The competitive advantage of a Hybrid / Direct Contact Heat Exchanger is strongest in applications where direct mixing is acceptable and where rapid heat transfer, simple structure, or difficult-media handling is important.
Design Selection Considerations
Media Compatibility
The first design question is whether the media can be mixed. Engineers should evaluate chemical compatibility, product formulation, contamination risks, phase behavior, and downstream separation. Steam, water, process gases, and selected liquid media may be suitable, but each case requires confirmation.
Flow Rate and Temperature Difference
Flow rates determine the contact volume, inlet size, velocity, pressure drop, and required residence time. The temperature difference determines the driving force and the amount of each medium required. An accurate energy balance should be prepared before equipment sizing.
Pressure Drop and Hydraulic Stability
The system should operate within a pressure range that supports stable flow without excessive energy consumption. High velocity can cause noise, vibration, erosion, and water hammer. Low velocity may result in poor mixing or incomplete condensation. Pumps, control valves, piping, and downstream equipment must be evaluated together with the exchanger.
Corrosion and Material Selection
Material selection should account for process fluids, dissolved gases, chlorides, cleaning agents, temperature, pressure, and operating cycles. Carbon steel may be cost-effective for suitable noncorrosive services, while stainless steel may be necessary for food, beverage, pharmaceutical-related, or corrosive applications.
Cleaning and Inspection
Although the equipment avoids a large tube bundle, it still requires a maintenance plan. The design should include appropriate access, drains, vents, inspection points, and cleaning connections. Food and biopharmaceutical applications may require clean-in-place compatibility, defined surface finishes, and documented sanitation procedures.
Control and Instrumentation
Temperature sensors should be positioned where they accurately represent the mixed outlet stream. Pressure transmitters, flowmeters, level instruments, control valves, and alarms may be required. Automated control can regulate the ratio of hot and cold media and prevent operation outside the design envelope.
Installation, Commissioning, and Operation
Before installation, the connection positions and media flow directions should be checked against the approved drawings. Reverse installation can cause poor mixing, unstable pressure, ineffective drainage, or incorrect control behavior. The shell should be mounted on properly aligned supports, with sufficient access for inspection and maintenance.
Piping should be independently supported so that excessive external loads are not transferred to the exchanger nozzles. Flanges should be aligned without forced assembly. Gaskets must be suitable for the pressure, temperature, chemical environment, and hygiene requirements. Bolts should be tightened evenly to the specified torque.
Commissioning should begin with a visual inspection and confirmation that all drains, vents, instruments, valves, and safety devices are correctly installed. The system should be flushed or cleaned according to the process requirements. Flow should be introduced gradually, and pressure and temperature should be increased in a controlled manner.
Sudden changes in steam flow or liquid flow can create thermal shock, water hammer, vibration, or unstable operation. Operators should monitor inlet and outlet temperatures, pressure, flow rate, noise, vibration, and condensate behavior during the initial run.
Operating parameters should remain within the approved design range. Exceeding the maximum flow rate can increase pressure drop and vibration. Excessive temperature can damage gaskets, accelerate corrosion, or affect product quality. Insufficient flow may lead to incomplete contact or poor temperature uniformity.
Maintenance and Troubleshooting
Uneven Media Mixing
Uneven mixing may be caused by an incorrect inlet flow rate, unsuitable injection angle, blocked distribution devices, or an incorrect ratio between the media. Operators should verify the flowmeters, inspect the inlet arrangement, check for deposits, and compare actual operating conditions with the design basis.
Vibration or Excessive Noise
Vibration or noise may result from excessive flow velocity, unstable two-phase flow, water hammer, cavitation, loose shell supports, or poorly aligned piping. The first response should be to check operating conditions and support integrity. Sudden valve closure and improper steam admission should be investigated carefully.
Shell Connection Leakage
Leakage at a flange may be caused by an aged or damaged gasket, uneven bolt tightening, flange deformation, corrosion, or external piping loads. The equipment should be depressurized and made safe before inspection. Gaskets should be replaced with approved materials, flange faces should be checked, and bolts should be tightened according to the specified sequence and torque.
Corrosion or Deposits
Corrosion may indicate unsuitable material selection, aggressive water chemistry, contamination, or inadequate drainage. Deposits may result from suspended solids, scaling minerals, chemical reactions, or insufficient cleaning. Regular inspection and process-water monitoring can help identify problems before they affect performance.
Long-Term Shutdown
When the equipment will remain idle for an extended period, internal media should be drained according to the process and safety procedures. Low-temperature environments require protection against freezing. The shell should be dried or preserved as appropriate to reduce corrosion. Open connections should be protected from dust, moisture, and foreign material.
Why Supplier Capability Matters
Selecting a direct contact heat exchanger is not only a matter of choosing shell dimensions. The supplier must understand the process, the media, the installation environment, and the consequences of direct mixing. A supplier with engineering, fabrication, quality-control, and international service capabilities can reduce project risk from the initial inquiry through commissioning.
Shiloc (Shanghai) Industrial Trading Co., Ltd. provides process systems and equipment for the food and beverage, biopharmaceutical, daily chemical, and fine chemical industries. Its product and service scope includes heat exchangers, aseptic mixing equipment, equipment manufacturing, import and export agency services, and engineering and technical support.
The company’s manufacturing and service model combines customized design with practical project coordination. Customers can communicate process requirements, receive technical recommendations, coordinate materials and fabrication, review documentation, and arrange international delivery through one service organization. This can be particularly useful for overseas buyers managing language, logistics, inspection, and technical coordination across borders.
The company emphasizes innovative design, process optimization, safe and efficient equipment, reliable supply, traceability, and personalized customer service. Its stated values include integrity, pragmatism, innovation, development, excellent quality, and global sharing. These principles are relevant to equipment projects where product performance depends on cooperation between the end user, process engineer, fabricator, installer, and operator.
For international procurement, the supplier’s ability to manage documentation is also important. Drawings, material certificates, welding records, inspection reports, pressure-test results, operating manuals, packing lists, and shipping documents should be coordinated with the customer’s project schedule. Clear documentation supports installation, validation, maintenance, and future replacement planning.
Project Workflow from Inquiry to Delivery
A typical project begins with a technical inquiry containing the media type, flow rate, inlet and outlet temperatures, operating and design pressure, required material, connection standards, installation conditions, and applicable industry requirements. Photographs, process flow diagrams, utility information, and space limitations can further improve the accuracy of the proposal.
The engineering stage converts these inputs into a preliminary design. This may include a heat balance, equipment arrangement, shell dimensions, nozzle locations, support details, instrumentation list, material specification, and estimated performance. If the application involves direct steam heating, the steam quality and condensate destination should be defined clearly.
After technical confirmation, manufacturing drawings and inspection requirements are reviewed. The production phase includes material preparation, forming, welding, machining, polishing, assembly, testing, and final inspection. Any customer witness points or third-party inspection requirements should be scheduled in advance.
Before shipment, the equipment should be protected against mechanical damage, moisture, contamination, and corrosion. Flange faces and instrument connections should be capped or sealed. Lifting points and center-of-gravity information should be made available to support safe unloading and installation.
After delivery, technical support may include installation guidance, operating recommendations, troubleshooting, spare-parts coordination, and service communication. A complete project approach helps ensure that the equipment delivers its expected benefit within the wider process system.
Frequently Asked Questions
Q1: What is the main advantage of a Hybrid / Direct Contact Heat Exchanger?
The main advantage is that it transfers heat through direct contact between compatible media, reducing the thermal resistance associated with a conventional tube or plate wall. It can also combine mixing and heat transfer in one operation.
Q2: Can the equipment replace every shell-and-tube or plate heat exchanger?
No. Direct contact equipment is suitable only when the media can be mixed safely or when an effective recovery and separation process is available. Shell-and-tube and plate exchangers remain preferable when the hot and cold streams must remain completely separated.
Q3: Is direct steam heating suitable for food and beverage processes?
It can be suitable for process water, cleaning water, and other applications where steam condensate may enter the liquid stream. Steam quality, product requirements, hygiene standards, and contamination control must be verified before selection.
Q4: Can the equipment be used in biopharmaceutical facilities?
It may be used for suitable utility, cleaning, sanitization-support, or process-development applications. Product-contact and high-purity water applications require detailed evaluation of material quality, surface finish, drainability, cleaning, validation, and regulatory requirements.
Q5: What materials are available?
Carbon steel and stainless steel are available according to media characteristics and process requirements. The specific stainless-steel grade, gasket material, surface finish, and auxiliary component materials should be selected through a corrosion, hygiene, and temperature review.
Q6: Does the equipment require internal tube cleaning?
No tube bundle is used as the primary heat transfer surface, so tube cleaning is not required. However, the shell, inlets, distribution devices, drains, and outlets should still be inspected and cleaned according to the media and operating conditions.
Q7: Can the shell length and pressure rating be customized?
Yes. Length, diameter, pressure rating, material, connection arrangement, support configuration, and instrumentation can be configured according to flow rate, temperature, pressure, installation, and process requirements.
Q8: What causes uneven outlet temperature?
Common causes include incorrect flow ratios, unsuitable inlet angles, blocked distribution devices, insufficient residence time, unstable pressure, or operation outside the design range. Flowmeters, inlet components, and actual operating conditions should be checked.
Q9: How can vibration and water hammer be reduced?
Flow rates should remain within the design range, steam should be admitted gradually, supports should be secure, and condensate should drain correctly. Piping layout, valve operation, pressure fluctuations, and cavitation should also be reviewed.
Q10: What information should be provided when requesting a quotation?
Useful information includes media names and composition, flow rates, inlet and outlet temperatures, operating and design pressure, allowable media mixing, material requirements, connection standards, cleaning methods, installation conditions, applicable codes, and required documentation.
Q11: How does the equipment support energy recovery?
It can transfer heat directly from steam, condensate, hot process water, or waste gas to a compatible receiving medium. The actual recovery benefit depends on the temperature levels, flow rates, utility costs, and design of the complete recovery system.
Q12: What makes a manufacturer suitable for international projects?
A suitable manufacturer should provide process engineering, controlled fabrication, material and weld traceability, inspection documentation, reliable packing, export coordination, technical communication, and after-sales support. These capabilities help reduce risks during cross-border procurement and installation.
Conclusion
The Hybrid / Direct Contact Heat Exchanger offers a practical alternative to conventional indirect heat exchange in processes where hot and cold media can be mixed safely. By eliminating the primary heat transfer wall, it reduces thermal resistance and can provide rapid heating, cooling, condensation, and gas treatment. Its integrated mixing function, simple internal arrangement, configurable pressure-resistant shell, and adaptability to selected difficult media create advantages over traditional equipment in appropriate applications.
For food and beverage manufacturers, it can support process-water heating, steam condensation, condensate recovery, cleaning utilities, and waste gas cooling. For biopharmaceutical and related facilities, it may serve selected utility, cleaning, sanitization-support, and process-development duties subject to strict review of hygiene, validation, purity, and contamination-control requirements.
The technology should be selected through a complete process evaluation rather than by heat duty alone. Media compatibility, flow distribution, pressure stability, corrosion resistance, drainage, cleaning, instrumentation, and downstream separation all influence successful operation. The best equipment design is one that balances thermal performance, safety, maintainability, regulatory expectations, and total cost of ownership.
Manufacturing quality is equally important. Precision fabrication, qualified welding, controlled polishing, material traceability, pressure testing, dimensional inspection, and complete documentation help convert a sound concept into dependable process equipment. With its Shanghai manufacturing facility, technical team, European and Danish design influence, and international trade and engineering capabilities, Shiloc (Shanghai) Industrial Trading Co., Ltd. is positioned to provide customized Hybrid / Direct Contact Heat Exchanger solutions for customers seeking reliable process systems and equipment.
As industrial manufacturers continue to pursue energy efficiency, simplified process lines, flexible production, and lower maintenance costs, direct contact heat exchange is likely to remain an important technology for compatible applications. When supported by responsible engineering and advanced manufacturing, it can help plants improve thermal performance while creating a more integrated and efficient process design.
References
1. Perry’s Chemical Engineers’ Handbook, sections on heat transfer, process equipment, fluid flow, and condensation.
2. Incropera, F. P., et al., Fundamentals of Heat and Mass Transfer, principles of convective heat transfer and phase-change heat transfer.
3. Coulson and Richardson’s Chemical Engineering, Volume 6, design of chemical engineering equipment and process systems.
4. ASME Boiler and Pressure Vessel Code, guidance related to pressure-containing equipment design, fabrication, examination, and testing.
5. European hygienic engineering guidance concerning the design, fabrication, surface finish, cleanability, and inspection of food-processing equipment.
6. Good Manufacturing Practice principles for food, beverage, pharmaceutical, and biopharmaceutical production facilities.
7. Industrial steam-system engineering references covering direct steam heating, condensation, condensate recovery, water hammer, and steam quality.
8. Industrial wastewater and exhaust-gas treatment references covering direct-contact cooling, gas-liquid contact, scrubbing, mist elimination, and corrosion control.
9. Manufacturer-provided technical information for Hybrid / Direct Contact Heat Exchangers, including operating principles, materials, applications, maintenance guidance, and customization capabilities.
Product: Hybrid / Direct Contact Heat Exchanger
PREV:Sanitary Steam Ejectors and Injectors for Food and Biopharmaceutical Process Systems
NEXT:No next article
NEXT:No next article
Interested in cooperation or have questions?
Recommended LINS
✦
Food and Beverage Process System
Food Processing Skid System
CIP Skid System for Food Industry
food and beverage process skid system
hygienic process skid for food industry
CIP process skid system for food industry
automated process skid system for food processing
modular food processing skid system
beverage processing skid system
food processing equipment skid system
Let'S Work Together Welcome Aboard!
-

haikexin@haikexin.com
+8613391278930
-
 +86-21-57560276
-
 No. 2819, Sihu Road,Fengxian District, Shanghai, China
Join Our Mailing List
Copyright © Shiloc (Shanghai) Industrial Trading Co., Ltd. All Rights Reserved.
Process Systems & Equipment For Food & Biopharma Manufacturers
